High-temperature plasma technologies that support the decarbonisation of energy-intensive sectors while maintaining process performance and operational reliability.
Plasma electrification and clean hydrogen for steel.
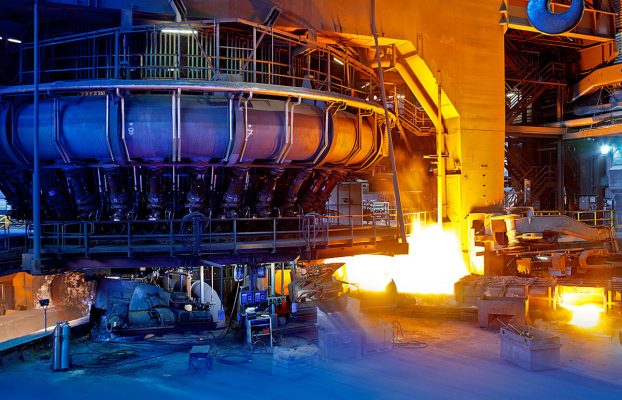
The steel industry accounts for about 7 % of global greenhouse gas emissions and about 11 % of global CO₂, largely because blast furnaces (BF-BOF) rely on metallurgical coal and still generate nearly 90 % of the sector’s emissions. Plenesys brings two complementary technologies:
AC plasma torch electrification can be integrated into blast furnace operations, including the EasyMelt process developed with strategic partners such as Paul Wurth. Powered by low-carbon electricity and compatible with coke oven gas (COG) reuse, it can reduce direct CO₂ emissions by up to 60 % while lowering CAPEX and OPEX and remaining compatible with existing installations.
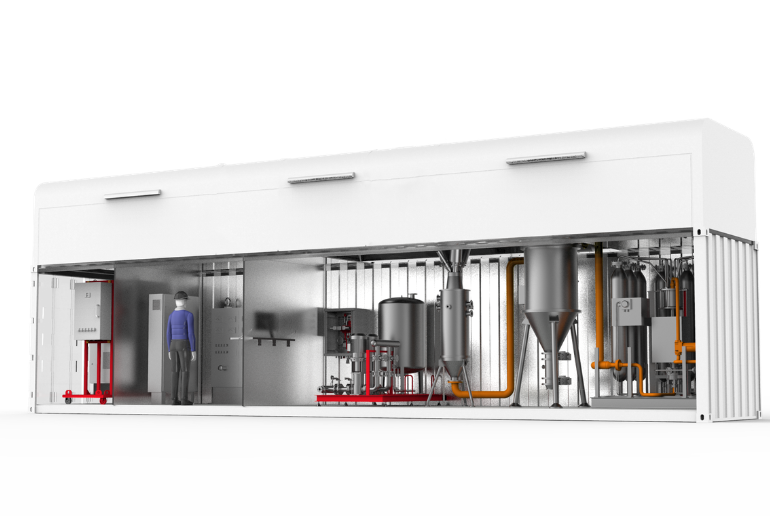
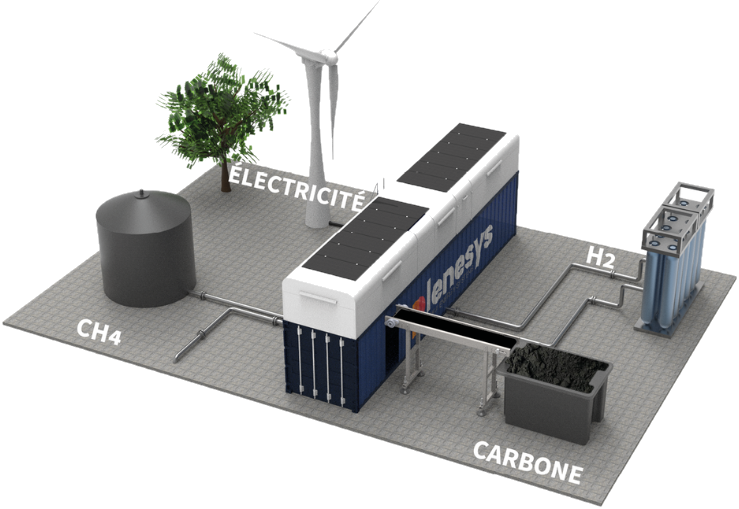
HyPlasma® supports direct reduction (DR) routes by supplying low-carbon hydrogen produced via methane pyrolysis — a scalable alternative to fossil-based reducing agents on the way to competitive fossil-free steel.
ALUMINIUM
Replacing the burner, not the furnace.
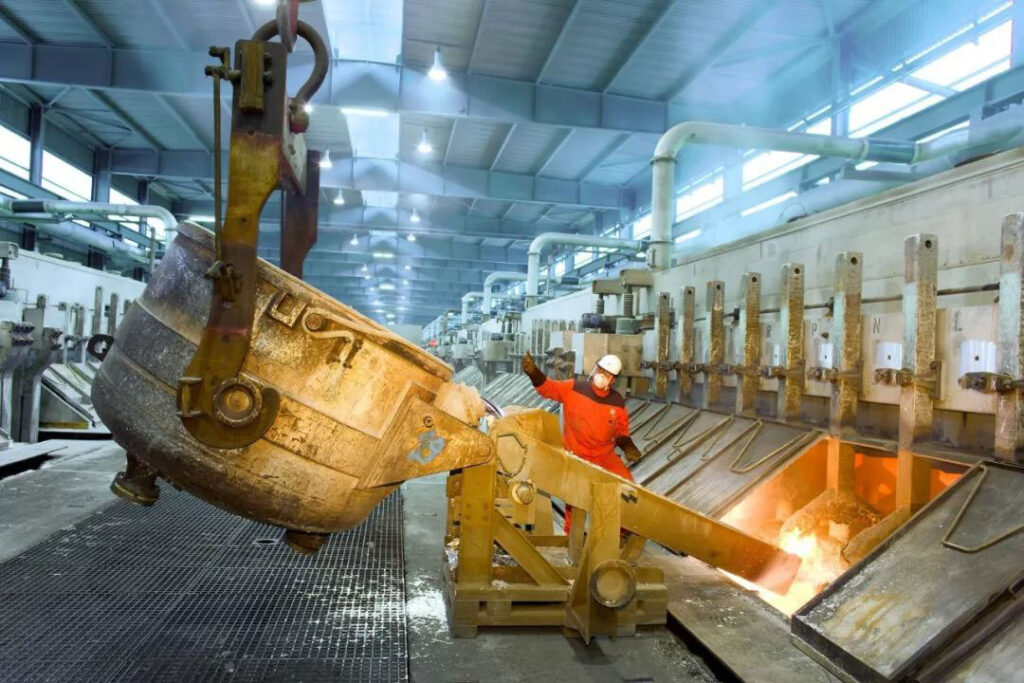
The aluminium industry relies on fossil-fuel thermal energy — mainly natural gas and fuel oil — at every high-temperature stage: digestion and calcination of aluminium hydroxide at 950–1,100 °C in alumina refining, and scrap drying, preheating, melting and holding in secondary production, with flame temperatures above 1,500 °C.
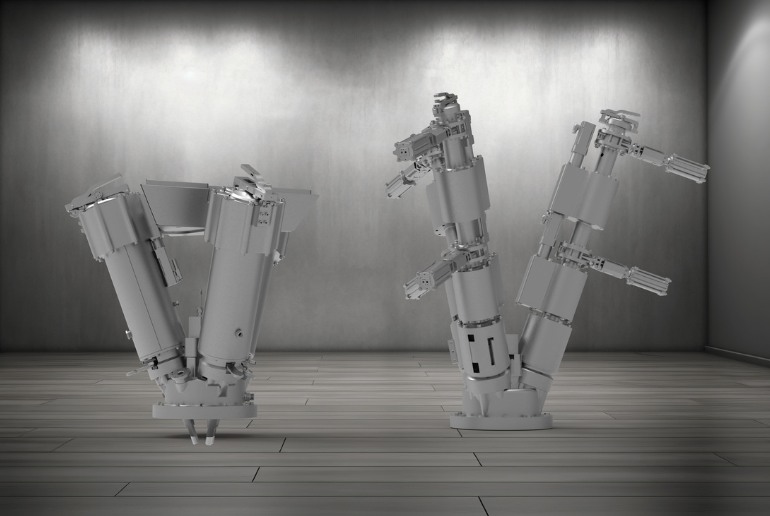
Plenesys’ plasma torch provides high-temperature heat from low-carbon electricity, without combustion. Replacing fossil burners in alumina refining, aluminium recycling and downstream thermal processes removes direct CO₂ at the point of use, as well as fuel-related NOₓ and SOₓ. Fully compatible with existing furnaces and renewable power, it enables CO₂ reductions of 20–30 % depending on plant configuration.
Reference: “Meeting net-zero emissions using plasma technology”, International Aluminium Journal.
CEMENT
A combustion-free burner for the clinker kiln.
Clinker production is the most CO₂-intensive stage of cement manufacturing: limestone and clay are heated to around 1,450 °C in a rotary kiln, accounting for more than 70 % of a plant’s CO₂. Roughly one third comes from fuel combustion — mainly coal and petroleum coke — and two thirds from limestone calcination.
The plasma torch offers a high-temperature, combustion-free alternative to fossil burners, delivering precisely controlled heat with stable thermal profiles and kiln stability, deployable within existing kiln configurations. Calcination emissions remain, but replacing fossil fuels with plasma heating can reduce total CO₂ by approximately 30 %, depending on configuration and integration strategy.
Reference: “Decarbonization of cement production by electrification”, ScienceDirect.